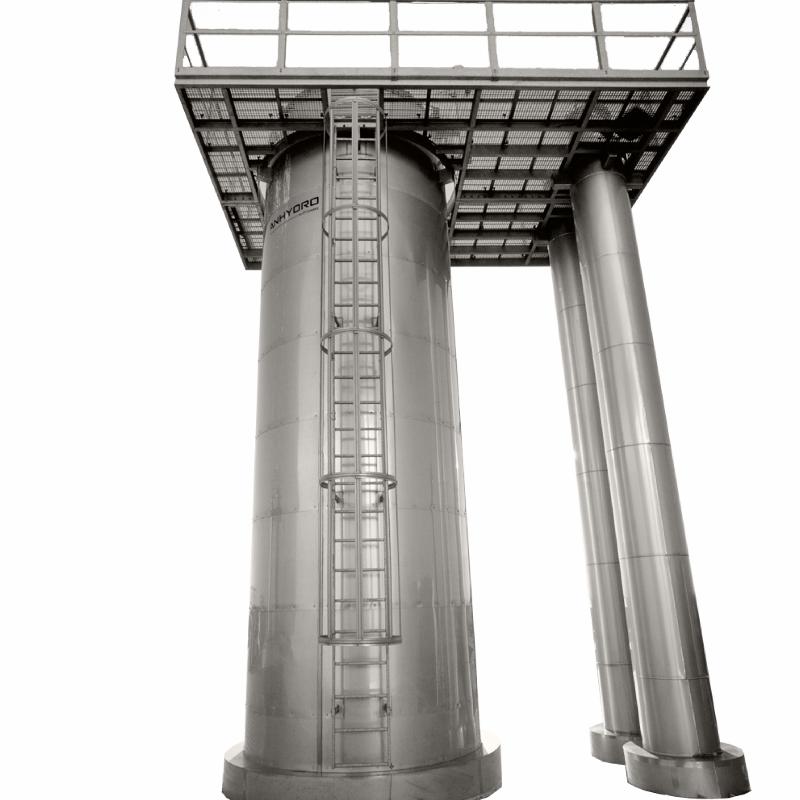
Anhydro Evaporators
arrow_backTo the overviewMaximum concentration. Minimum energy consumption.
Anhydro evaporators help manufacturers concentrate liquids efficiently while reducing energy costs and maximizing product quality. Designed for dairy, food, beverage and pharmaceutical applications, the portfolio includes tubular, plate, TVR and MVR evaporator technologies tailored to specific processing requirements.
Combining advanced energy recovery, flexible configurations and decades of process expertise, Anhydro solutions deliver reliable performance for a wide range of products, from low-viscosity liquids to more demanding applications. Custom-designed systems help producers optimize operations, improve efficiency and reduce total cost of ownership.
Key benefits:
Energy-efficient concentration and evaporation
Flexible solutions for a wide range of products and capacities
TVR and MVR technologies for reduced utility consumption
Gentle processing of heat-sensitive products
Custom-engineered systems optimized for specific applications
Advanced process modelling for maximum performance
Comprehensive lifecycle support and aftermarket services
To learn more, visit us at FoodTech 2026, Stand 9654 in Hall M.

This product is added by:
Anhydro
Anhydro drying and evaporation technologies help manufacturers produce consistent powders, concentrate liquids and improve energy efficiency. From individual equipment to complete turnkey systems, our solutions combine decades of thermal processing expertise with advanced automation and application support for better process control.
At FoodTech 2026, see Anhydro SmartDry™, which automatically keeps your spray dryer close to its optimal point, and Anhydro BlueLight™, which whitens lactose without activated carbon.
Test before you invest: our food technologists can help you develop and tr
Responsibility for content on this site
Information, images, product descriptions, videos, certifications, sustainability claims, and other content on company profiles are uploaded and maintained by the individual exhibitors.
Exhibitors are solely responsible for ensuring that their content is accurate, properly documented, and legally compliant, including compliance with applicable regulations concerning marketing, sustainability claims, and intellectual property rights.
MCH A/S solely provides the platform and does not, as a general rule, verify the content.