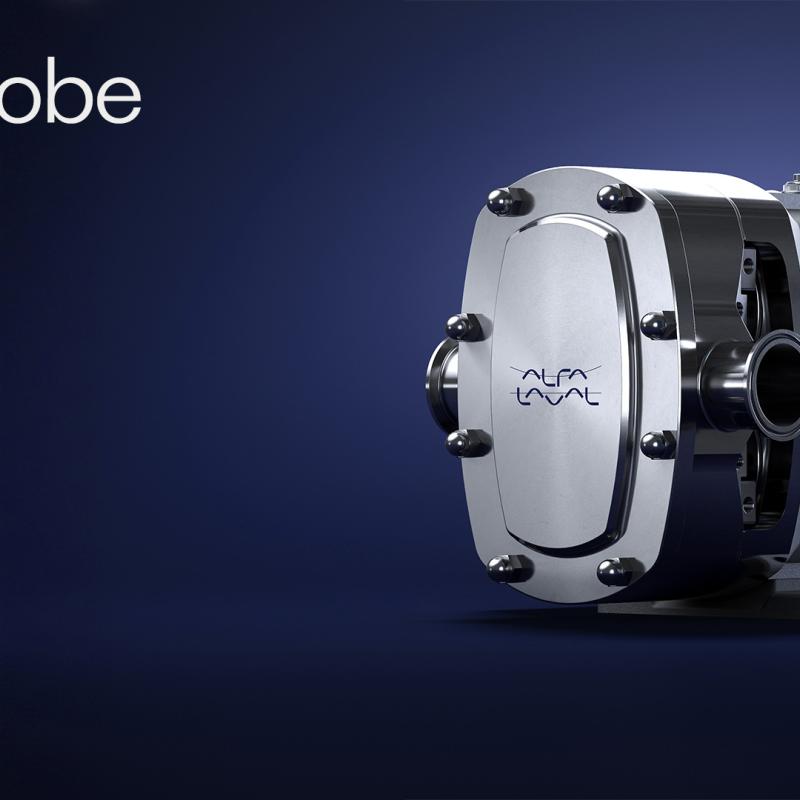
Alfa Laval MaxiLobe is a hygienic rotary lobe pump that combines high volumetric efficiency with gentle product handling, reliable operation and easy maintenance.
MaxiLobe is designed for manufacturers in the dairy, food and beverage industries, among others, where product quality, hygiene and operational efficiency are essential.
Higher Capacity – Lower Energy Consumption
Thanks to its improved pump design, MaxiLobe can deliver the required flow at lower operating speeds. This enables energy savings of more than 25% in many applications while reducing shear stress on sensitive products.
Compared to the previous Alfa Laval SRU series, MaxiLobe delivers at least 5% higher flow rates under defined operating conditions. Its high efficiency may also allow for a smaller pump size, helping to reduce both investment and operating costs.
Hygienic Design and Easy Maintenance
MaxiLobe is EHEDG and 3-A certified and designed for excellent cleanability and high standards of food safety. Front-loading mechanical seals can be replaced without removing the pump from the process line, simplifying maintenance and reducing the risk of extended downtime.


This product can be seen at the exhibition.
This product can be seen at the Exhibition

This product is added by:
Iversen Trading
Flow components with integrity – we know you and your process
At iversen trading, we have been working with flow since 1975. We advise on and supply pumps, valves, heat exchangers, instrumentation and other flow components to Danish industry – with a particularly strong focus on the food, beverage and process industries.
But to us, process equipment is not just about technology, specifications and part numbers. It is also about understanding the production environment in which the components need to perform.
We believe in honest advice, doing business properly and building long-term r
Responsibility for content on this site
Information, images, product descriptions, videos, certifications, sustainability claims, and other content on company profiles are uploaded and maintained by the individual exhibitors.
Exhibitors are solely responsible for ensuring that their content is accurate, properly documented, and legally compliant, including compliance with applicable regulations concerning marketing, sustainability claims, and intellectual property rights.
MCH A/S solely provides the platform and does not, as a general rule, verify the content.